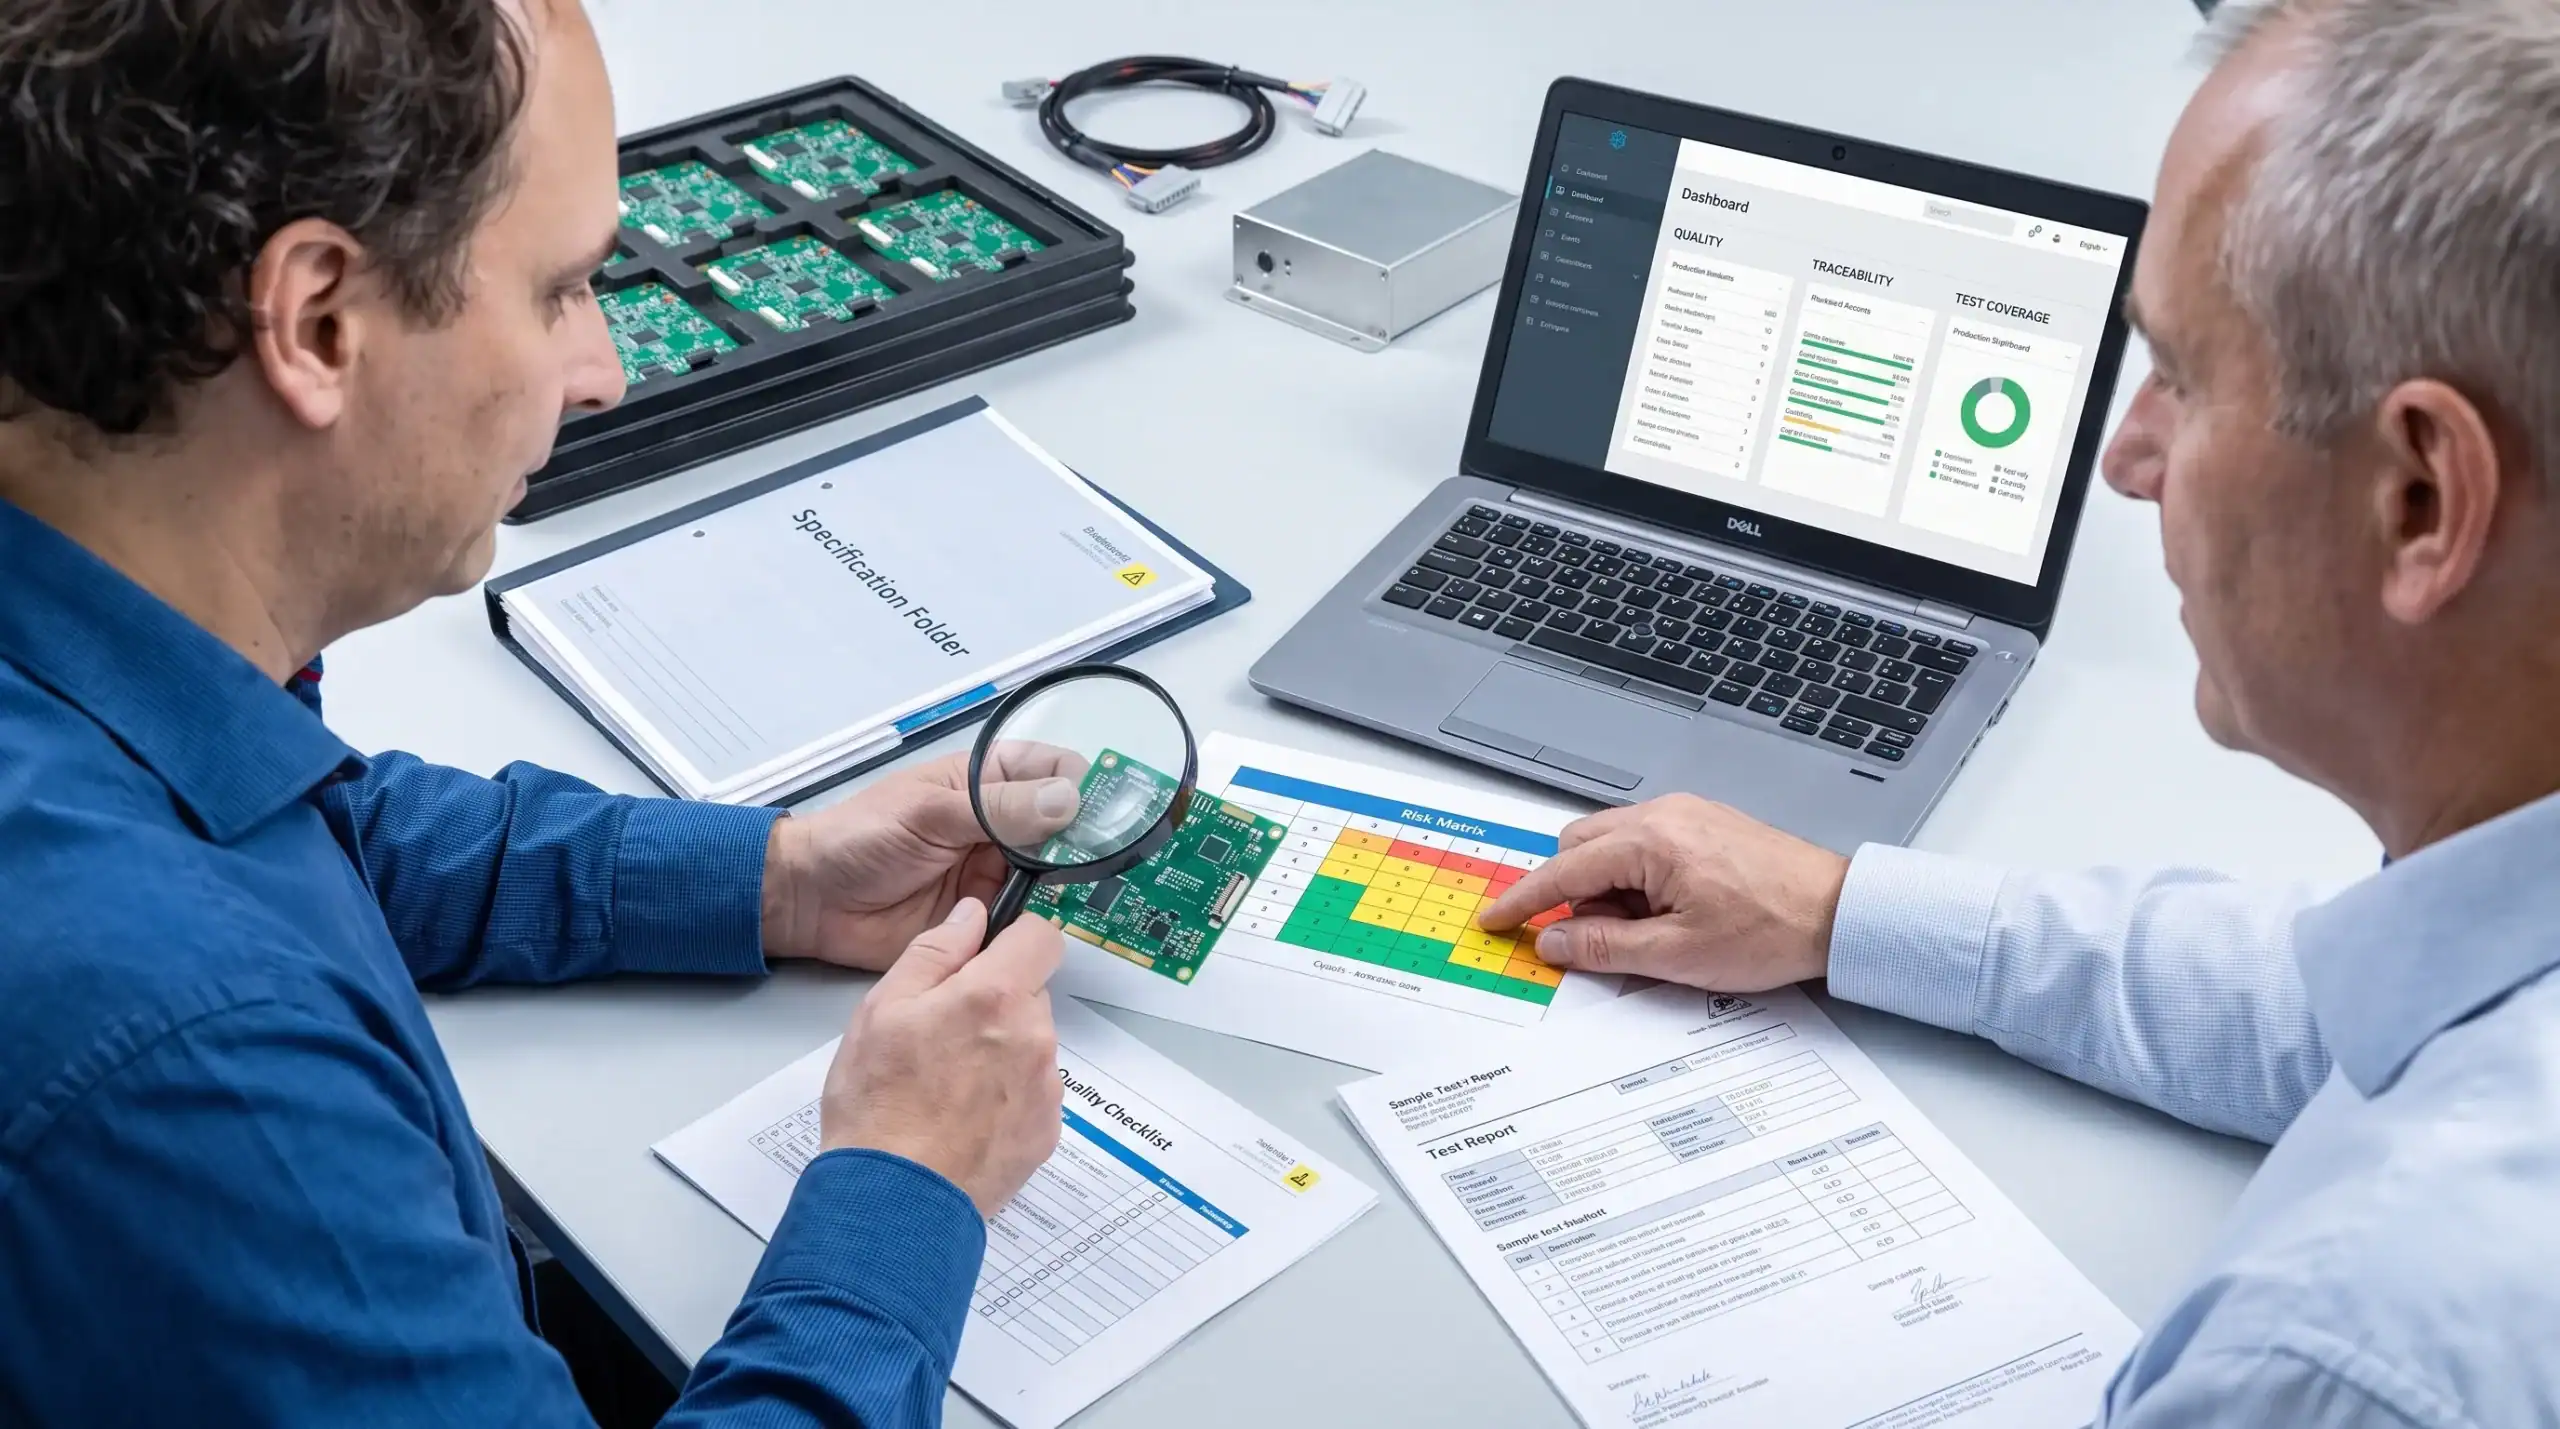
Choosing between electronic assembly services Ltd options is rarely a simple purchasing exercise. For a defence sensor, maritime control unit, robotics drive, connected machine module or automotive subsystem, the assembly partner can influence reliability, certification risk, field performance and long-term serviceability.
A search for “electronic assembly services ltd” may bring up companies with similar names, broad electronics manufacturing service providers and smaller PCB assembly specialists. The legal suffix tells you very little. What matters is whether the supplier can handle the technical risk profile of your product, not just place components on a board.
For engineering managers, CTOs and product owners, the assessment should start earlier than the quotation stage. A capable partner will want to understand the operating environment, compliance route, expected lifetime, production volumes, failure consequences and test strategy before promising a unit price. If they do not ask those questions, they may be optimising for assembly efficiency while leaving product risk untouched.
Start by defining the product risk, not the assembly task
Many supplier comparisons begin with a bill of materials, Gerber files and a request for lead time. That is understandable, but it can hide the most important question: what must this electronic product survive in real life?
A simple consumer accessory, a motor control module inside an industrial machine and a marine-connected sensor may all involve PCB assembly, yet they require different levels of engineering judgement. Vibration, humidity, heat rise, electromagnetic interference, enclosure constraints, connector strain, firmware programming and operator misuse can all affect assembly decisions.
Before approaching suppliers, document the context around the product. This does not need to be a 100-page specification, but it should make the risk visible. Include expected volumes, environmental conditions, duty cycle, power levels, communication interfaces, regulatory markets, service expectations and what happens if the product fails.
This step is especially important when comparing an assembly-only supplier with an engineering-led development partner. The first may be very efficient once the design is stable. The second can help identify whether the design is actually ready to be assembled, tested and scaled.
Match the supplier type to your development stage
Not every electronics supplier should be judged by the same criteria. Some companies are excellent at high-volume manufacturing of mature designs. Others are better suited to prototypes, design-for-manufacture feedback or complex embedded product development. The right choice depends on where your product sits in the development lifecycle.
| Supplier type | Best suited for | Main assessment question |
|---|---|---|
| PCB assembly specialist | Stable board designs, prototypes or limited production | Can they assemble consistently and provide useful process feedback? |
| Electronics manufacturing service provider | Mature products moving into repeat production | Can they control quality, sourcing, traceability and throughput? |
| Engineering-led electronics partner | Products still evolving technically | Can they reduce design, compliance and manufacturing risks before production? |
| Full contract manufacturer | Established products with defined production documentation | Can they manage volume, logistics, quality systems and lifecycle support? |
If your internal team already has a validated design, clear test procedures and controlled documentation, a strong assembly partner may be enough. If the product still has unresolved EMC, thermal, analogue, firmware or power electronics questions, you should look for deeper engineering capability before committing to a manufacturing route.
Assess technical depth behind the quotation
A low quotation can be attractive, particularly when development budgets are under pressure. But for professional electronics, the cheapest early decision can create the most expensive later change. Re-spinning a PCB after EMC testing, changing connectors after field failures or redesigning power stages after thermal issues can cost far more than selecting a stronger partner from the start.
When reviewing electronic assembly services Ltd options, ask how the supplier handles technical review before production. A capable supplier should be able to discuss component placement constraints, solderability, thermal relief, clearance and creepage, connector accessibility, programming access, test points and mechanical integration. They do not need to redesign the full product unless that is part of the scope, but they should be able to identify manufacturability risks.
For a more PCB-specific view, ProMicro has also covered what to look for in PCB assembly services, including quality control, sourcing discipline and readiness for scale. In a broader supplier assessment, use those PCB factors as part of the evaluation, not as the whole decision.
A useful test is to ask each supplier to review a representative design package and provide written feedback. Look for practical comments, not generic reassurances. Strong feedback often includes specific layout concerns, alternative process recommendations, missing documentation, unclear tolerances or test access issues.
Look for design-for-manufacture and design-for-test discipline
Design for manufacture and design for test are not administrative steps. They shape how reliably a product can be built, inspected, programmed, calibrated and repaired.
For surface-mount assemblies, small layout choices can influence yield. Component spacing, panelisation, fiducials, paste aperture design and thermal mass distribution all matter. For products with power electronics, analogue sensing or high-speed communication, the assembly process must preserve the intent of the design rather than simply follow files blindly.
Design for test is equally important. In many professional products, a visual inspection and power-on check are not enough. The supplier may need to support in-circuit testing, boundary scan, firmware loading, serial number programming, functional test fixtures, calibration routines or environmental screening.
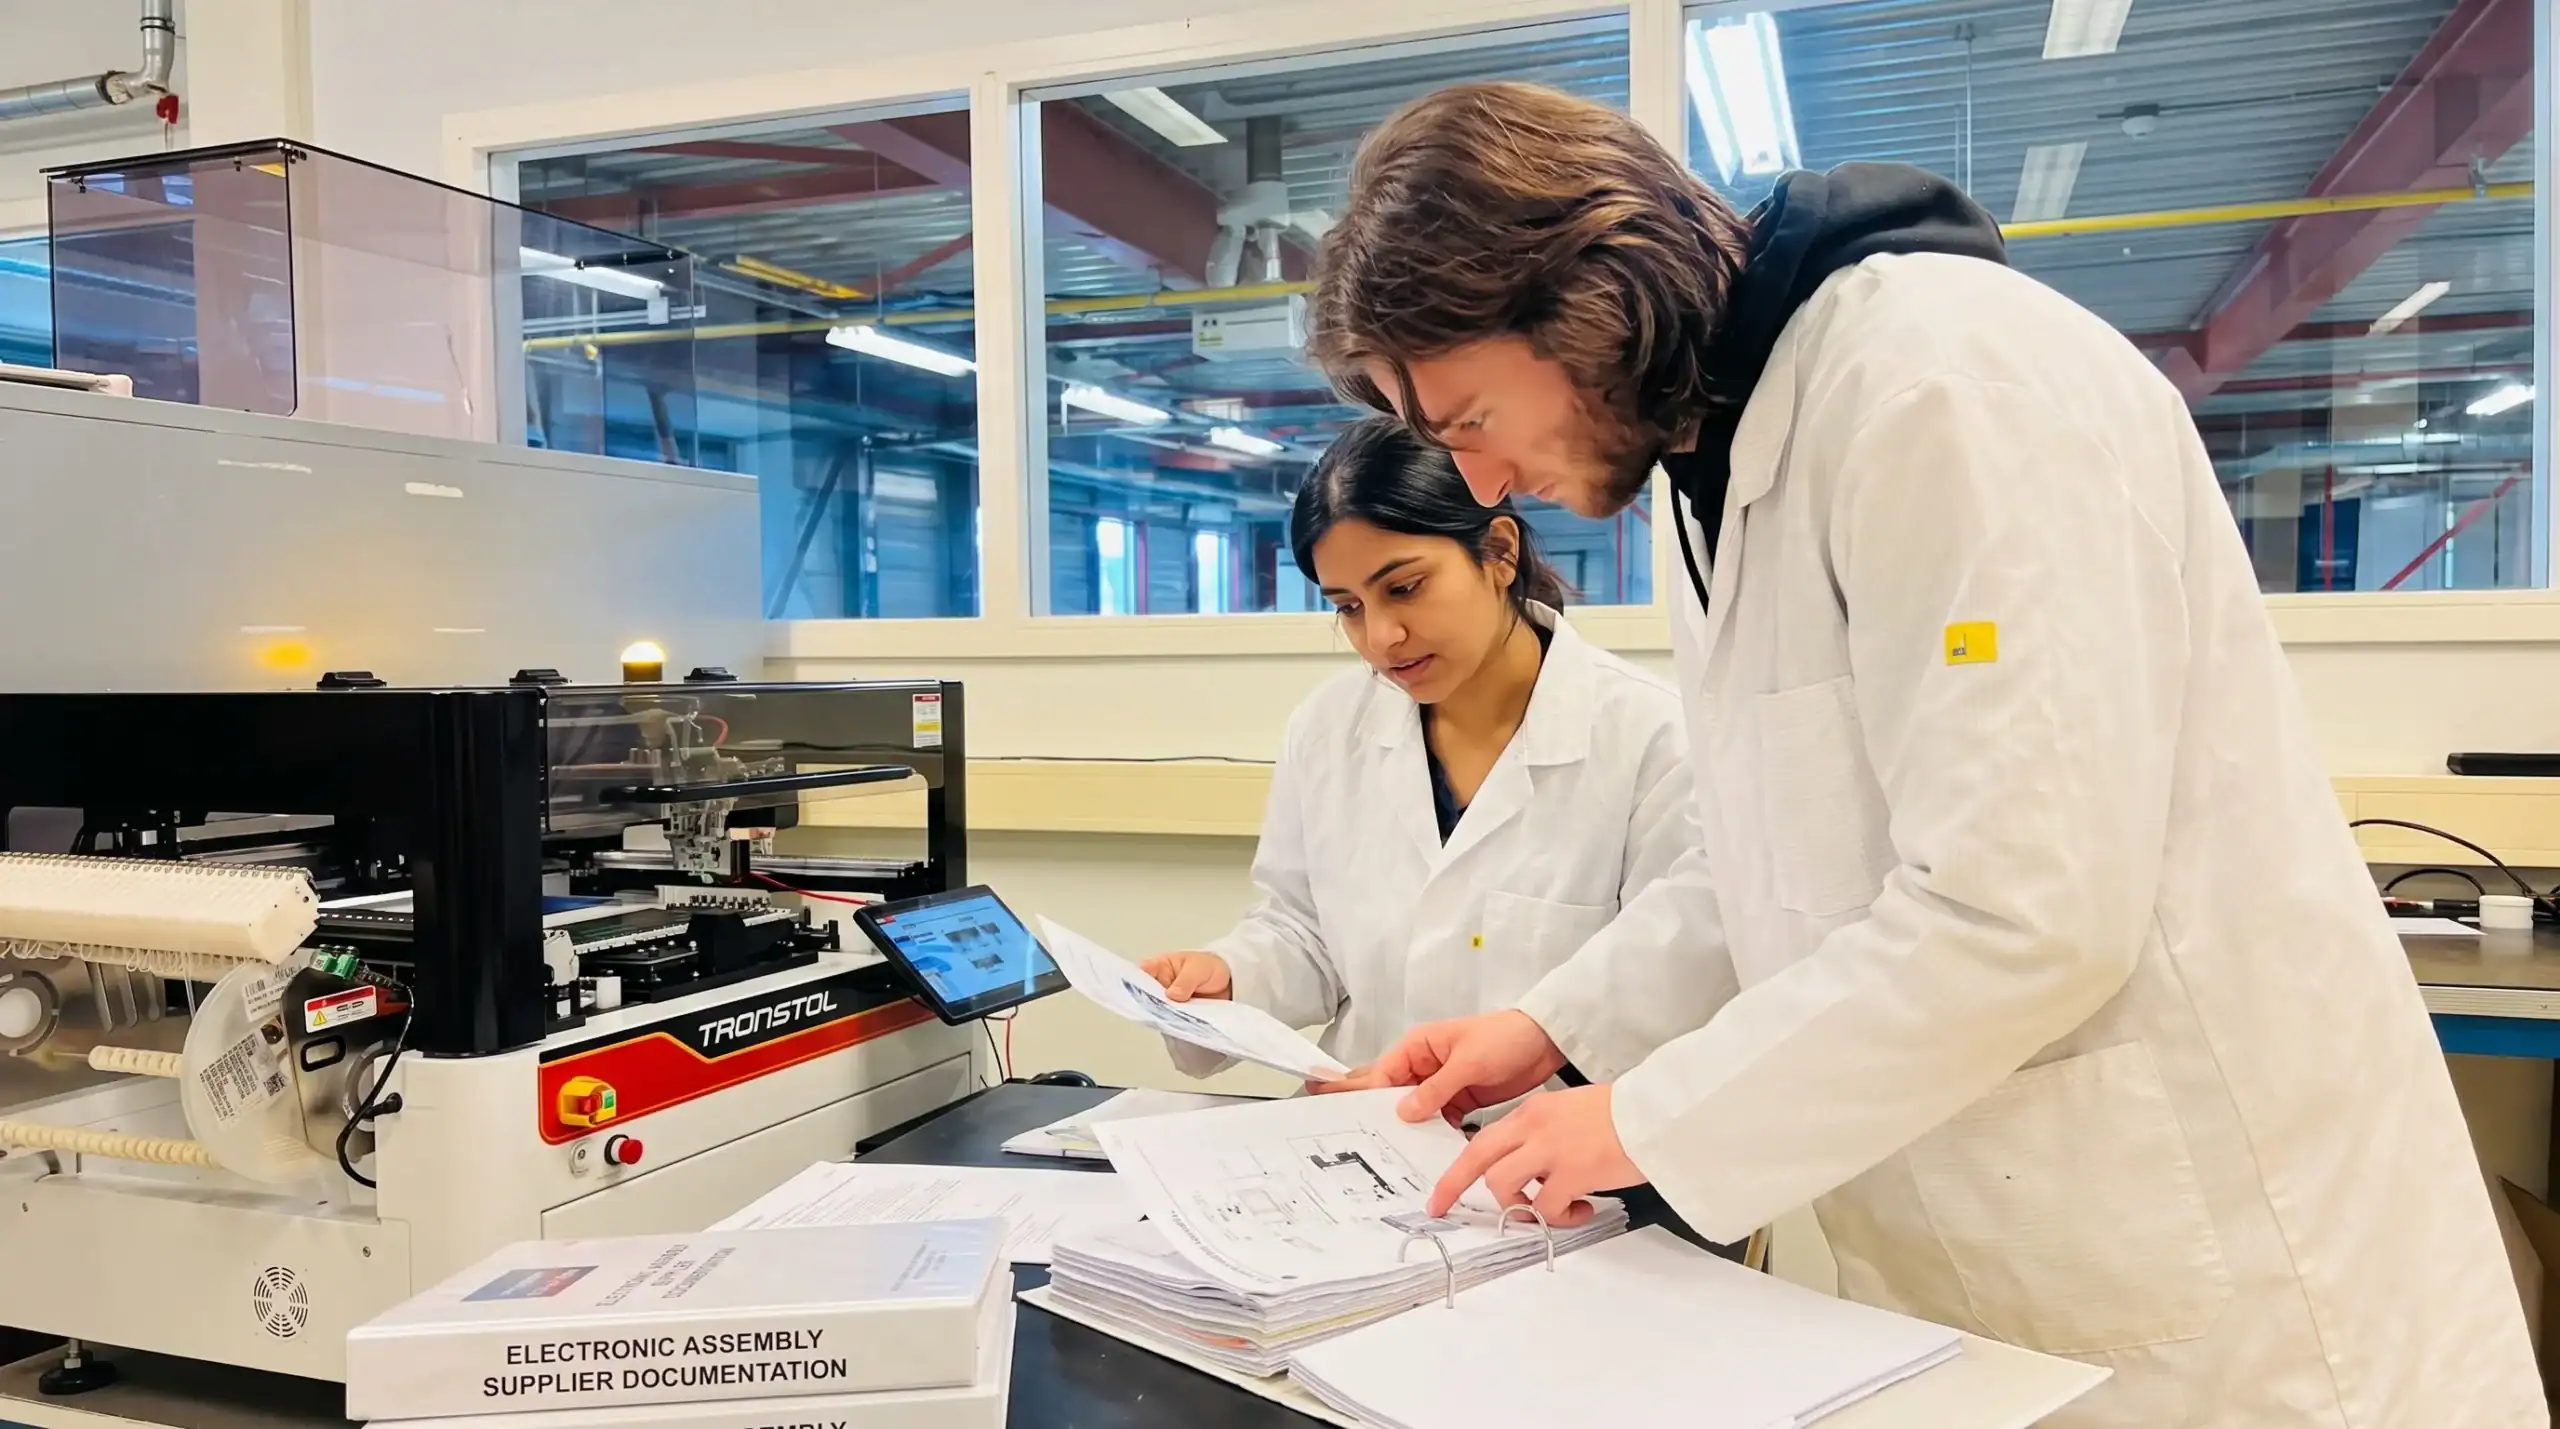
Ask how test coverage is agreed. A mature supplier should be comfortable discussing failure modes, acceptance criteria, test data retention and escalation paths. For safety-related or high-value equipment, also ask how non-conforming units are handled and whether corrective actions are documented.
Check quality systems, traceability and process control
Quality is often presented through certificates, but certificates alone do not prove that a supplier is right for your product. They are a starting point. You need to understand how quality is translated into daily production behaviour.
Evidence may include ISO 9001 certification, IPC-A-610 workmanship criteria, IPC J-STD-001 soldering practices, incoming inspection procedures, ESD controls, calibration records and controlled rework processes. Depending on your sector, you may need additional controls around traceability, documentation, cybersecurity, export restrictions or safety-critical design reviews.
Ask suppliers how they trace components, batches, operators, inspection results and test data. For low-volume high-value products, this can be just as important as for larger production runs. If a failure appears in the field, traceability helps determine whether the issue is isolated, process-related, component-related or design-related.
This is where assembly and engineering overlap. ProMicro explains the relationship between production steps and reliability in its article on electronics assembly steps that shape product quality. The practical lesson is clear: quality planning starts before the assembly line, not after the first failures.
Evaluate compliance awareness early
Many products are assembled correctly but still struggle during compliance testing. EMC, RED, CE marking, UKCA, electrical safety and sector-specific requirements are affected by design choices made long before formal testing begins.
An assembly supplier does not need to be a notified body or certification laboratory. However, they should understand how assembly decisions can affect compliance risk. Cable routing, shielding, grounding, enclosure bonding, component substitutions, power supply choices and RF module integration can all influence the final result.
Be cautious if a supplier treats compliance as something that happens only at the end. For connected products, RED considerations may affect radio modules, antennas, firmware behaviour and documentation. For power electronics, thermal design and safety spacing can influence both reliability and conformity. For industrial and maritime environments, EMC robustness is often central to field performance.
The strongest partners will not guarantee certification casually. Instead, they will design and assemble with compliance in mind, recommend pre-compliance testing where appropriate and maintain discipline around component changes.
Review supply chain and component substitution practices
Component availability remains a serious concern for electronics programmes. Even when global shortages ease, obsolescence, allocation, counterfeit risk and long lead times can disrupt production.
A good supplier should be able to explain how they source components, approve alternatives and protect against unauthorised substitutions. This is particularly important for analogue electronics, power devices, sensors, wireless modules and safety-related components, where a “similar” part can change product behaviour.
Ask whether the supplier can support approved vendor lists, lifecycle checks, last-time-buy planning and redesign discussions when parts become unavailable. If your product is expected to stay in the market for many years, lifecycle management should be part of the evaluation from the start.
For complex products, sourcing should not be separated from engineering. A purchasing decision can affect noise performance, thermal margin, firmware compatibility or compliance. The supplier should know when a substitute is commercially acceptable and when engineering review is required.
Include embedded software, connectivity and mechanical interfaces
Electronic assembly is not isolated from the rest of the product. Many modern products combine embedded software, sensors, motor drives, wireless communication, IoT connectivity and enclosure design. A supplier that only looks at the PCB may miss interface risks.
For example, programming access may conflict with enclosure design. A wireless module may pass bench testing but perform poorly once placed inside a metal housing. A motor drive may work in a lab but create interference inside a larger machine. A connector may be easy to solder yet difficult to service in the final installation.
Some products also extend beyond the embedded system. If the hardware is part of a connected product with mobile onboarding, diagnostics or an operator interface, assess how your electronics partner will exchange test data, firmware requirements and interface assumptions with software teams. For standalone app development or MVP validation alongside a hardware programme, a specialist cross-platform mobile app developer can be useful, provided ownership of interfaces, firmware dependencies and acceptance criteria is clear.
The key point is integration. The right assembly route should support the full product architecture, not create a handover gap between electronics, firmware, enclosure and external software.
Use a structured scoring matrix
A structured scoring matrix helps avoid decisions based only on the most persuasive sales conversation or the lowest unit price. It also gives technical and commercial stakeholders a shared basis for comparison.
| Assessment area | What to check | Why it matters |
|---|---|---|
| Product understanding | Supplier asks about environment, duty cycle, compliance and failure impact | Shows whether they understand hidden requirements |
| Technical capability | DFM, DFT, power, analogue, firmware and mechanical awareness | Reduces late design changes and integration issues |
| Quality control | Inspection, test records, ESD, rework and non-conformance handling | Supports repeatable production and field reliability |
| Compliance awareness | EMC, RED, CE marking, UKCA and safety-related design implications | Lowers risk before formal testing |
| Supply chain control | Approved sources, substitution rules and lifecycle planning | Protects continuity and product consistency |
| Communication | Clear feedback, issue tracking and escalation behaviour | Prevents silent risk accumulation |
| Scale-up readiness | Prototype learning, production documentation and test fixture planning | Helps move from lab success to volume readiness |
Weight each area based on product risk. A low-cost consumer device may place more emphasis on throughput and cost control. A maritime, defence, robotics or industrial product should usually place more weight on reliability, traceability, test coverage and engineering collaboration.
Watch for supplier red flags
Red flags do not always mean a supplier is incapable. Sometimes they indicate a mismatch between your product needs and the supplier’s operating model. The earlier you spot that mismatch, the easier it is to avoid delays.
Common warning signs include:
- The supplier quotes before understanding the application environment.
- They focus only on price, lead time and placement capability.
- They accept incomplete documentation without raising questions.
- They have no clear process for component substitutions.
- Test strategy is treated as optional or left entirely to the customer.
- Compliance issues are dismissed as the responsibility of another party.
- Prototype feedback is informal and not captured for production learning.
- They cannot explain how quality records and traceability are maintained.
Also be cautious with suppliers that are excellent in one area but positioned as a complete solution without evidence. A strong PCB assembler may not be the right partner for system engineering. A contract manufacturer may not want to engage deeply in early design uncertainty. A design consultancy may not be set up for manufacturing support. The goal is not to find the biggest supplier, but the best fit for the product risk and maturity.
Decide whether you need an assembler or a development partner
The final decision often comes down to this distinction: are you buying assembly capacity or reducing product development risk?
If the design is mature, the test strategy is proven and your internal team can manage engineering issues, an assembly-focused supplier may be appropriate. If the product still contains technical uncertainty around embedded software, power electronics, analogue behaviour, sensors, wireless communication, EMC, enclosure integration or production readiness, an engineering-led partner is usually safer.
This distinction matters because many costly problems are created before assembly starts. Poor test access, marginal component choices, insufficient thermal margin, unclear firmware loading procedures or weak documentation may not show up in a simple quotation. They appear later, during certification, pilot builds, field trials or volume ramp-up.
A capable development partner should think beyond the immediate assignment. That does not mean adding unnecessary scope. It means identifying hidden requirements, documenting risks and helping your team make informed decisions before the cost of change increases.
Frequently asked questions
What should I ask electronic assembly services Ltd suppliers first? Start by asking how they review product risk before quoting. A strong supplier will ask about the operating environment, compliance markets, production volumes, test requirements, component sourcing and failure consequences.
Is the cheapest electronic assembly supplier usually a bad choice? Not necessarily. For a stable, low-risk design with complete documentation, a cost-efficient assembler can be the right choice. For complex electronics, price should be evaluated alongside technical review, quality control, test coverage and lifecycle support.
How do I know if my product is ready for assembly? Your product is closer to assembly readiness when the design files, bill of materials, approved component sources, programming method, test procedure, mechanical constraints and acceptance criteria are controlled. If these are still changing, engineering support may be needed before production.
Should an assembly supplier help with EMC or CE marking? They should not casually promise certification, but they should understand how assembly, layout, components, cabling, shielding and enclosure decisions can affect EMC, RED, CE marking and safety-related risks.
When should I choose an engineering-led partner instead of an assembly-only supplier? Choose an engineering-led partner when the product combines hardware, firmware, power electronics, analogue circuits, sensors, wireless communication or mechanical integration and when reliability, compliance or long-term manufacturing readiness are important.
Need an engineering-led view before choosing an assembly route?
If you are comparing electronic assembly services Ltd options for a professional product, the right decision is rarely based on assembly price alone. It depends on product risk, development maturity, compliance expectations, test strategy and the level of engineering support your internal team needs.
ProMicro supports companies from first idea through embedded system development, power and analogue electronics, PCB design, prototyping and preparation for volume manufacturing. If you need a partner who can look beyond the board and assess the full product context, you can discuss your development challenge with ProMicro’s electronics design team.