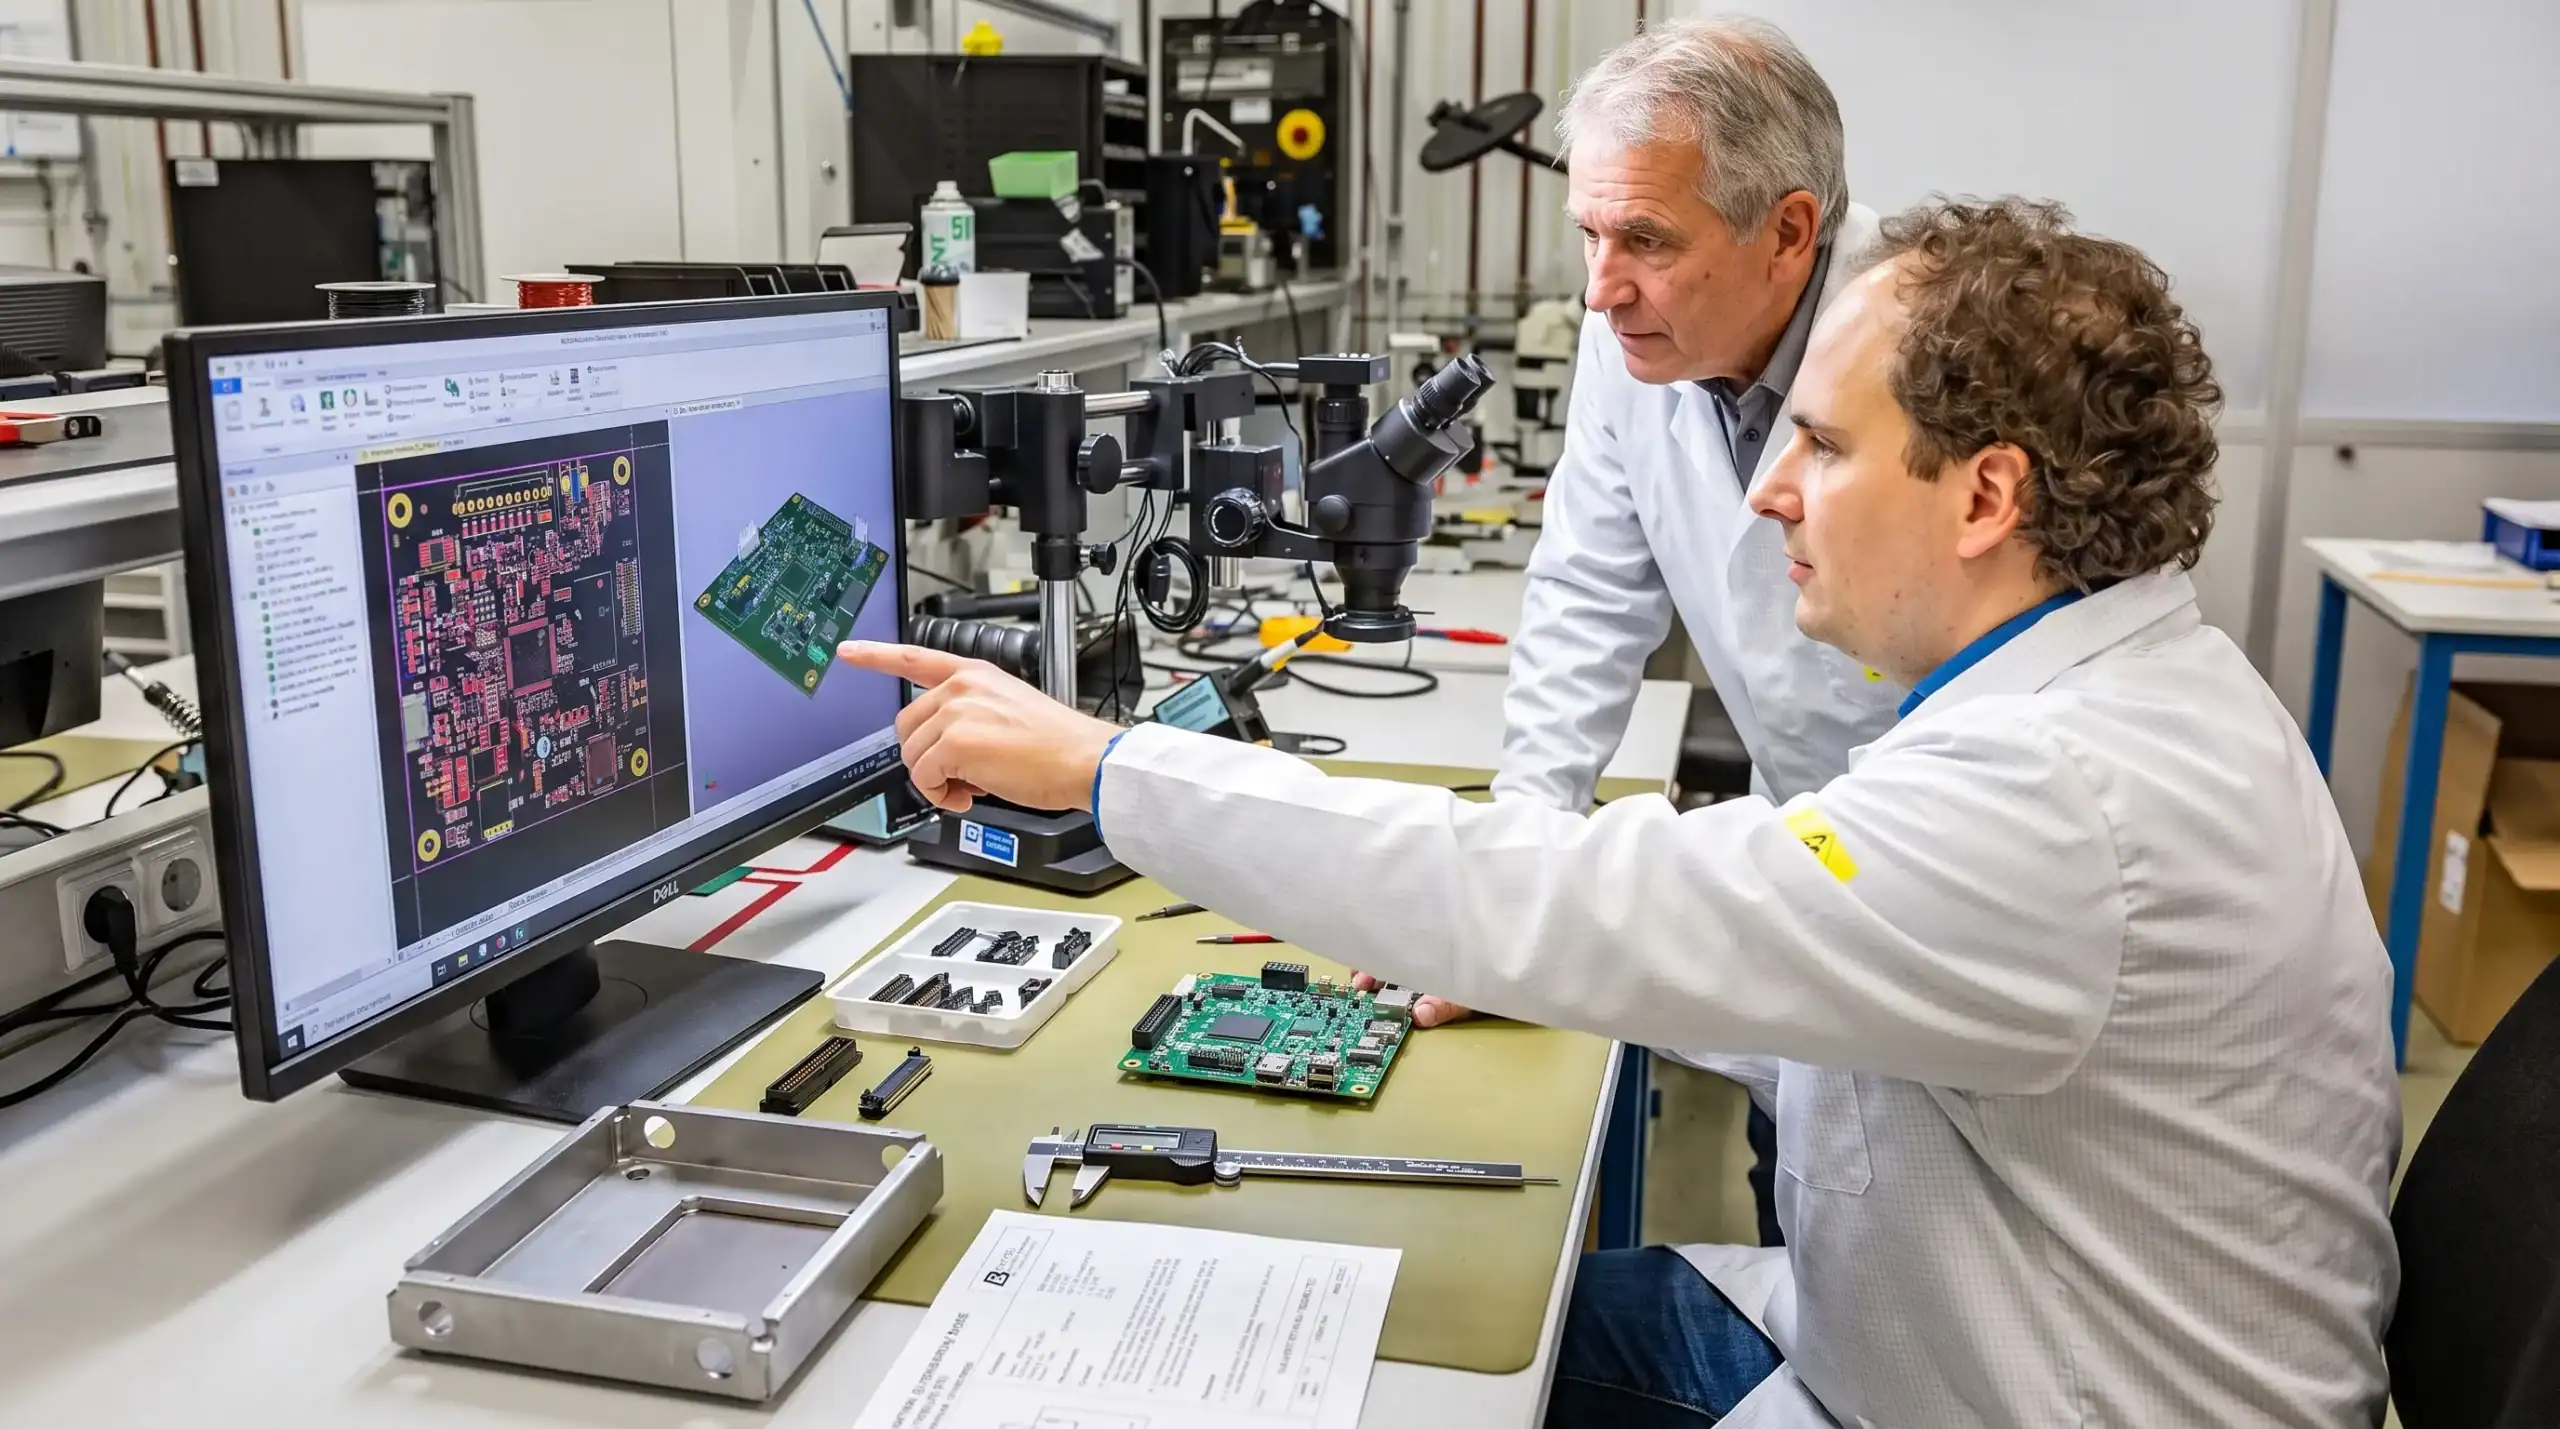
PCB CAD design is where a product idea becomes a set of manufacturing instructions. For professional electronics, that makes the CAD environment more than a drawing tool. It is the place where electrical intent, mechanical interfaces, thermal behaviour, EMC strategy, assembly requirements and long-term serviceability must come together before money is committed to fabrication.
Costly revision errors are rarely caused by one obvious mistake. More often, they come from small gaps that were not visible at the schematic or layout stage: a footprint copied from an old project, a clearance rule left as a default, a connector that fits the PCB but not the enclosure, a missing test point or a power path that works in the lab but overheats in a sealed product.
For machine builders, robotics companies, maritime systems, defence suppliers, automotive developers and high-tech manufacturers, a PCB respin can delay more than the board. It can affect firmware schedules, mechanical parts, test fixtures, certification planning and customer commitments. Strong CAD discipline reduces those risks early, when changes are still relatively inexpensive.
Why PCB CAD revision errors become expensive
A PCB revision is not just a new set of Gerbers. Once a board has moved into prototype testing or pilot production, each design change can ripple through procurement, assembly, firmware, enclosure design, test documentation and compliance work. If the product contains motor drives, wireless communication, sensors, analogue measurement circuits or high-current power electronics, the coupling between these disciplines becomes even stronger.
The earlier a design error is found, the easier it is to correct. A wrong component value in a schematic review may take minutes to fix. A wrong footprint discovered after assembly may cost boards, components, labour and schedule time. A return path problem discovered during EMC testing may require changes to stack-up, placement, routing and shielding strategy.
| Revision error | Typical CAD-related cause | Downstream impact |
|---|---|---|
| Incorrect footprint or pinout | Unverified library symbol, wrong package variant or incomplete datasheet check | Assembly failure, component rework or unusable prototypes |
| Inadequate creepage or clearance | Default spacing rules used for high-voltage or safety-related nets | Layout redesign, safety concerns or compliance delays |
| Poor return path control | Signal routing separated from reference planes or split-plane crossings | EMC problems, unstable measurements or communication errors |
| Connector misalignment | PCB layout not synchronised with enclosure and cable routing | Mechanical redesign, harness changes or field installation issues |
| Thermal weakness | Copper area, via strategy or component spacing not modelled early enough | Derating, reliability problems or enclosure temperature issues |
| Missing production test access | Test strategy added after layout completion | Slow debugging, expensive fixtures or poor manufacturing diagnostics |
The purpose of disciplined CAD practice is not to make the design process bureaucratic. It is to make important engineering assumptions visible, reviewable and enforceable.
Treat requirements as CAD constraints, not background notes
A common source of revision errors is the gap between written requirements and what the CAD system actually checks. If a clearance, impedance, current capacity or keepout zone is only described in a document, it depends on memory and manual review. If it is encoded in the CAD rules, the design can be checked continuously.
Good PCB CAD design starts before component placement. The engineering team should translate product requirements into rule sets and constraints that match the application environment. That includes operating voltage and current, isolation needs, thermal limits, vibration exposure, service access, cable interfaces, expected production volume and applicable compliance targets such as EMC, RED or CE-related requirements.
For example, a low-voltage sensor board for a laboratory device may tolerate layout choices that would be unacceptable in a motor controller mounted inside an industrial machine. A wireless product may need antenna keepouts, ground clearance rules and enclosure material awareness from the start. A maritime or defence application may demand stronger attention to connector retention, environmental sealing, power transients and maintainability.
The IPC standards, including widely used guidance such as IPC-2221 and IPC-7351, can help define spacing, land pattern and board design practices. They do not replace product-specific engineering judgement, but they give teams a recognised framework for avoiding avoidable CAD mistakes.
The most useful CAD rules usually include net classes for power, analogue, digital, safety-related and high-speed signals. They also include differential pair definitions, creepage and clearance rules, controlled impedance targets, polygon connection rules, via constraints, component height limits, mechanical keepouts and test point requirements.
Build component libraries that can be trusted
Library errors are among the most frustrating revision causes because they often look correct until the board is assembled. A schematic symbol can be electrically misleading. A footprint can match one package variant but not the part that purchasing actually orders. A 3D model can hide a height or connector position issue that becomes visible only when the PCB meets the enclosure.
A professional CAD library should be treated as controlled engineering data. Every new component needs a defined review process, especially when it is used in safety-related circuits, power stages, analogue front ends or production-critical interfaces. The review should compare the schematic symbol, footprint, pin mapping, recommended land pattern, courtyard, paste mask, solder mask, polarity marking, 3D body and approved manufacturer part numbers.
This is particularly important when equivalent components are allowed. A capacitor, MOSFET, connector or wireless module may appear interchangeable in the bill of materials, but have different pad geometry, height, thermal pad dimensions, pin plating, current rating or lifecycle status. CAD data should reflect the approved purchasing reality, not an idealised component from an early concept phase.
Library discipline also supports lifecycle management. When a product is expected to remain in production for years, component obsolescence and second-source planning cannot be separated from CAD data. Clear links between schematic symbols, footprints, manufacturer part numbers and approved alternatives make future revisions more predictable.
Keep schematics reviewable and unambiguous
Schematic quality has a direct impact on layout quality. A cluttered or inconsistent schematic makes it harder to spot wrong net names, swapped pins, missing pull-ups, unclear power domains or incorrect analogue grounding assumptions. It can also slow firmware, test and production teams that depend on the schematic for debugging.
For complex embedded systems, hierarchical schematics usually reduce ambiguity. Power input, regulation, analogue sensing, microcontroller, communications, motor control and safety interfaces should be separated into logical blocks. Net naming should be consistent enough that design intent is obvious during review and during PCB layout.
Electrical rule checks are useful, but they are not a substitute for engineering review. CAD tools can detect unconnected pins, conflicting output drivers and missing power flags. They cannot always understand whether a reset line needs a defined start-up state, whether an analogue reference is routed too close to a noisy switching node or whether a connector pinout matches the service technician's workflow.
A good schematic review asks practical questions. Can the product be programmed and tested after assembly? Are there enough measurement points for bring-up? Are power sequencing and brownout behaviour understood? Are unused pins handled according to the datasheet? Are field connections protected against realistic misuse? These questions prevent layout revisions later.
Use layout constraints to protect reliability and EMC
PCB layout is where many hidden risks become physical. Placement and routing decisions affect signal integrity, power integrity, thermal performance, manufacturability and EMC behaviour. For professional products, layout cannot be reduced to fitting tracks between pins.
Stack-up should be defined early and entered into the CAD environment with realistic material, copper thickness and impedance assumptions. Reference planes, return paths, controlled impedance layers and high-current copper areas need to be planned before routing begins. If stack-up is left until fabrication data export, the design may already contain routing decisions that are difficult to correct.
Placement should follow the functional architecture of the product. Power entry, protection, switching converters, motor drivers, analogue sensing, microcontrollers, wireless modules and connectors all create different constraints. Sensitive analogue circuits should not be forced to coexist with noisy switching loops without separation, reference planning and filtering strategy. High di/dt loops in power electronics should be compact and predictable. Connectors should support the mechanical and service context, not just the schematic.
Return paths deserve specific attention. A signal track is only half the current path. If the return current is forced around plane cuts, connector gaps or poorly placed vias, the board can become more susceptible to emissions, crosstalk and measurement instability. This is why PCB layout should be reviewed as part of the full electrical system, not as a cosmetic stage after schematic approval. ProMicro explores this wider relationship in more detail in its article on how PCB board design affects reliability and EMC.
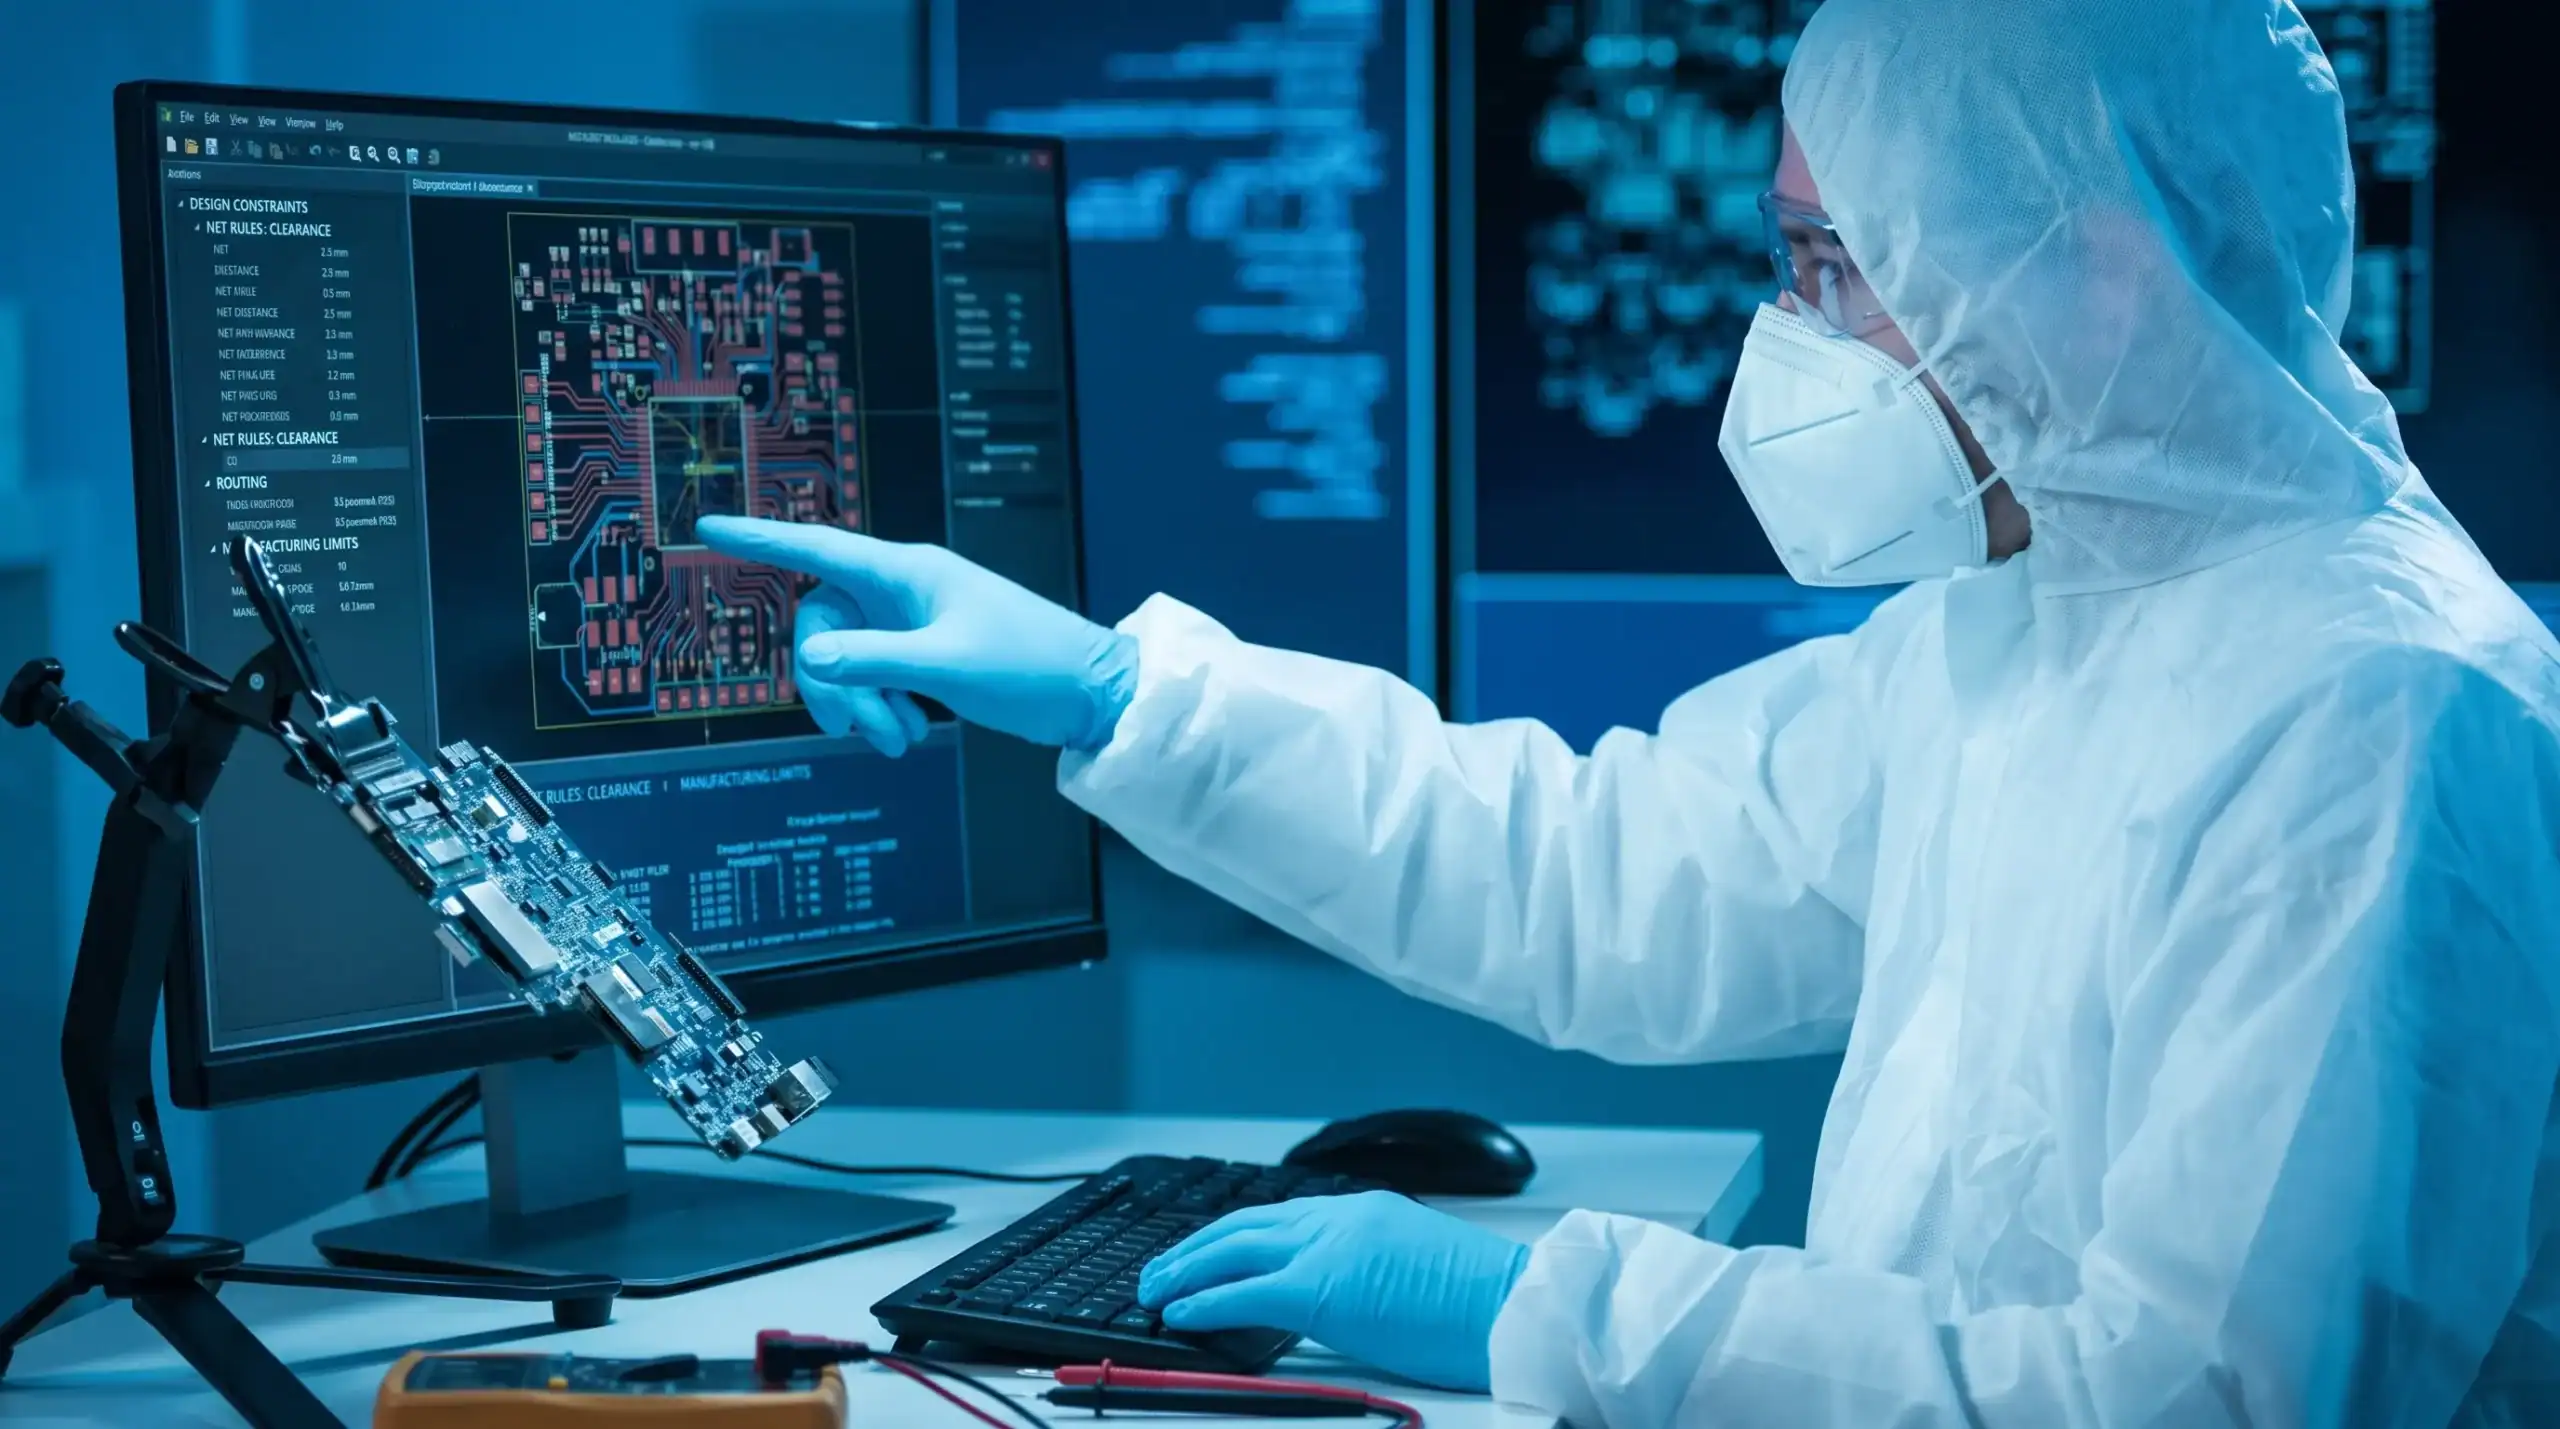
Synchronise PCB CAD with mechanical and enclosure design
Many revision errors are discovered when the PCB is physically integrated into the product. A board may be electrically correct, yet fail to fit the enclosure, align with connectors, provide service access or meet thermal expectations. In compact products, this risk increases because antennas, heat-generating components, displays, buttons, glands, cable bends and mounting hardware all compete for space.
ECAD and MCAD synchronisation should be part of the normal workflow. The PCB outline, mounting holes, connector positions, keepout zones, component heights and enclosure interfaces need controlled exchange between electronics and mechanical teams. A 3D model is not just a presentation asset. It is a design verification tool that can reveal collisions, tolerance issues and assembly access problems before prototype parts are ordered.
This matters strongly in machine manufacturing, robotics, maritime systems and automotive-related equipment, where the PCB often lives inside a larger electromechanical product. Cable routing, vibration, enclosure sealing, heat transfer and maintenance access can decide whether a design works reliably in the field.
Mechanical integration also influences EMC and safety. Connector placement affects cable emissions and susceptibility. Enclosure material influences shielding and antenna performance. Mounting points can create grounding opportunities or unwanted conductive paths. Treating the PCB as one part of a complete system prevents late corrections that are expensive to implement.
Build manufacturability into the CAD process
Manufacturability should not start after the layout is complete. If fabrication and assembly limits are considered only during data export, the team may discover that track widths, annular rings, solder mask slivers, via structures, component spacing or panelisation assumptions need changes.
A robust CAD workflow uses design rules that match the intended fabrication and assembly route. Prototype suppliers sometimes allow choices that are acceptable for a small batch but unsuitable for repeatable volume manufacturing. If a product is expected to scale, the CAD rules should reflect the target manufacturing process as early as possible.
| CAD practice | Revision risk reduced |
|---|---|
| Use manufacturer-aware track, gap, drill and annular ring limits | Fabrication rejection or yield problems |
| Define component courtyards and assembly clearances | Pick-and-place collisions or hand rework |
| Add test points during layout, not after routing | Poor production diagnostics and slow bring-up |
| Review stencil, paste mask and thermal pad strategy | Solder voiding, tombstoning or inconsistent assembly quality |
| Maintain clear fabrication and assembly drawings | Supplier interpretation errors |
| Keep BOM, placement data and CAD revision aligned | Wrong parts, wrong rotation or release confusion |
This is where design for manufacturing becomes an engineering discipline rather than a final checklist. The CAD model, component data, assembly documentation and test strategy should support each other. For a deeper manufacturing-focused view, ProMicro's design for manufacturing PCB checklist explains how early decisions affect reliable volume builds.
Control versions, variants and release packages
Revision errors often happen because the design files are correct in one place and outdated somewhere else. A schematic is updated but the PCB is not synchronised. A BOM is exported before a component change. A pick-and-place file uses an old rotation. A supplier receives Gerbers from one revision and an assembly drawing from another.
CAD data should be released as a controlled package, not as a loose collection of files. The package should identify the schematic revision, PCB revision, BOM revision, fabrication outputs, assembly outputs, test documents and any approved deviations. Once released, changes should move through a defined engineering change process.
This becomes especially important when a product has variants. A machine controller may share one base PCB across several customer configurations. A wireless product may have regional module variants. A power electronics platform may use different connector or current rating options. CAD variants can be useful, but only when options are clearly controlled and reflected in the BOM, assembly drawings and test procedures.
Version control does not need to slow development. It prevents teams from losing time to uncertainty. When a prototype fails, engineers need to know exactly which board, component set, firmware version and test configuration produced the result. Without that traceability, debugging becomes guesswork.
Use staged design reviews before ordering boards
A single final review is rarely enough for complex electronics. By the time a layout is complete, many choices have become interdependent. Staged reviews make it easier to catch errors when the cost of change is still low.
A practical review flow can include these gates:
- Requirements and architecture review, to confirm product context, operating environment, compliance targets and major technical risks.
- Library and schematic review, to verify symbols, footprints, pin mapping, power domains, protection circuits and test access.
- Placement and stack-up review, to assess EMC strategy, thermal paths, mechanical integration and manufacturability before detailed routing.
- Routing and pre-release review, to check constraints, return paths, clearances, documentation and production data consistency.
The reviewers should include more than the PCB layout engineer. Embedded software, mechanical engineering, production, test and system engineering perspectives often reveal issues that pure layout review misses. For example, a firmware engineer may need access to debug pins after enclosure assembly. A production engineer may identify a connector that is difficult to inspect. A system engineer may question whether a cable interface is protected for field conditions.
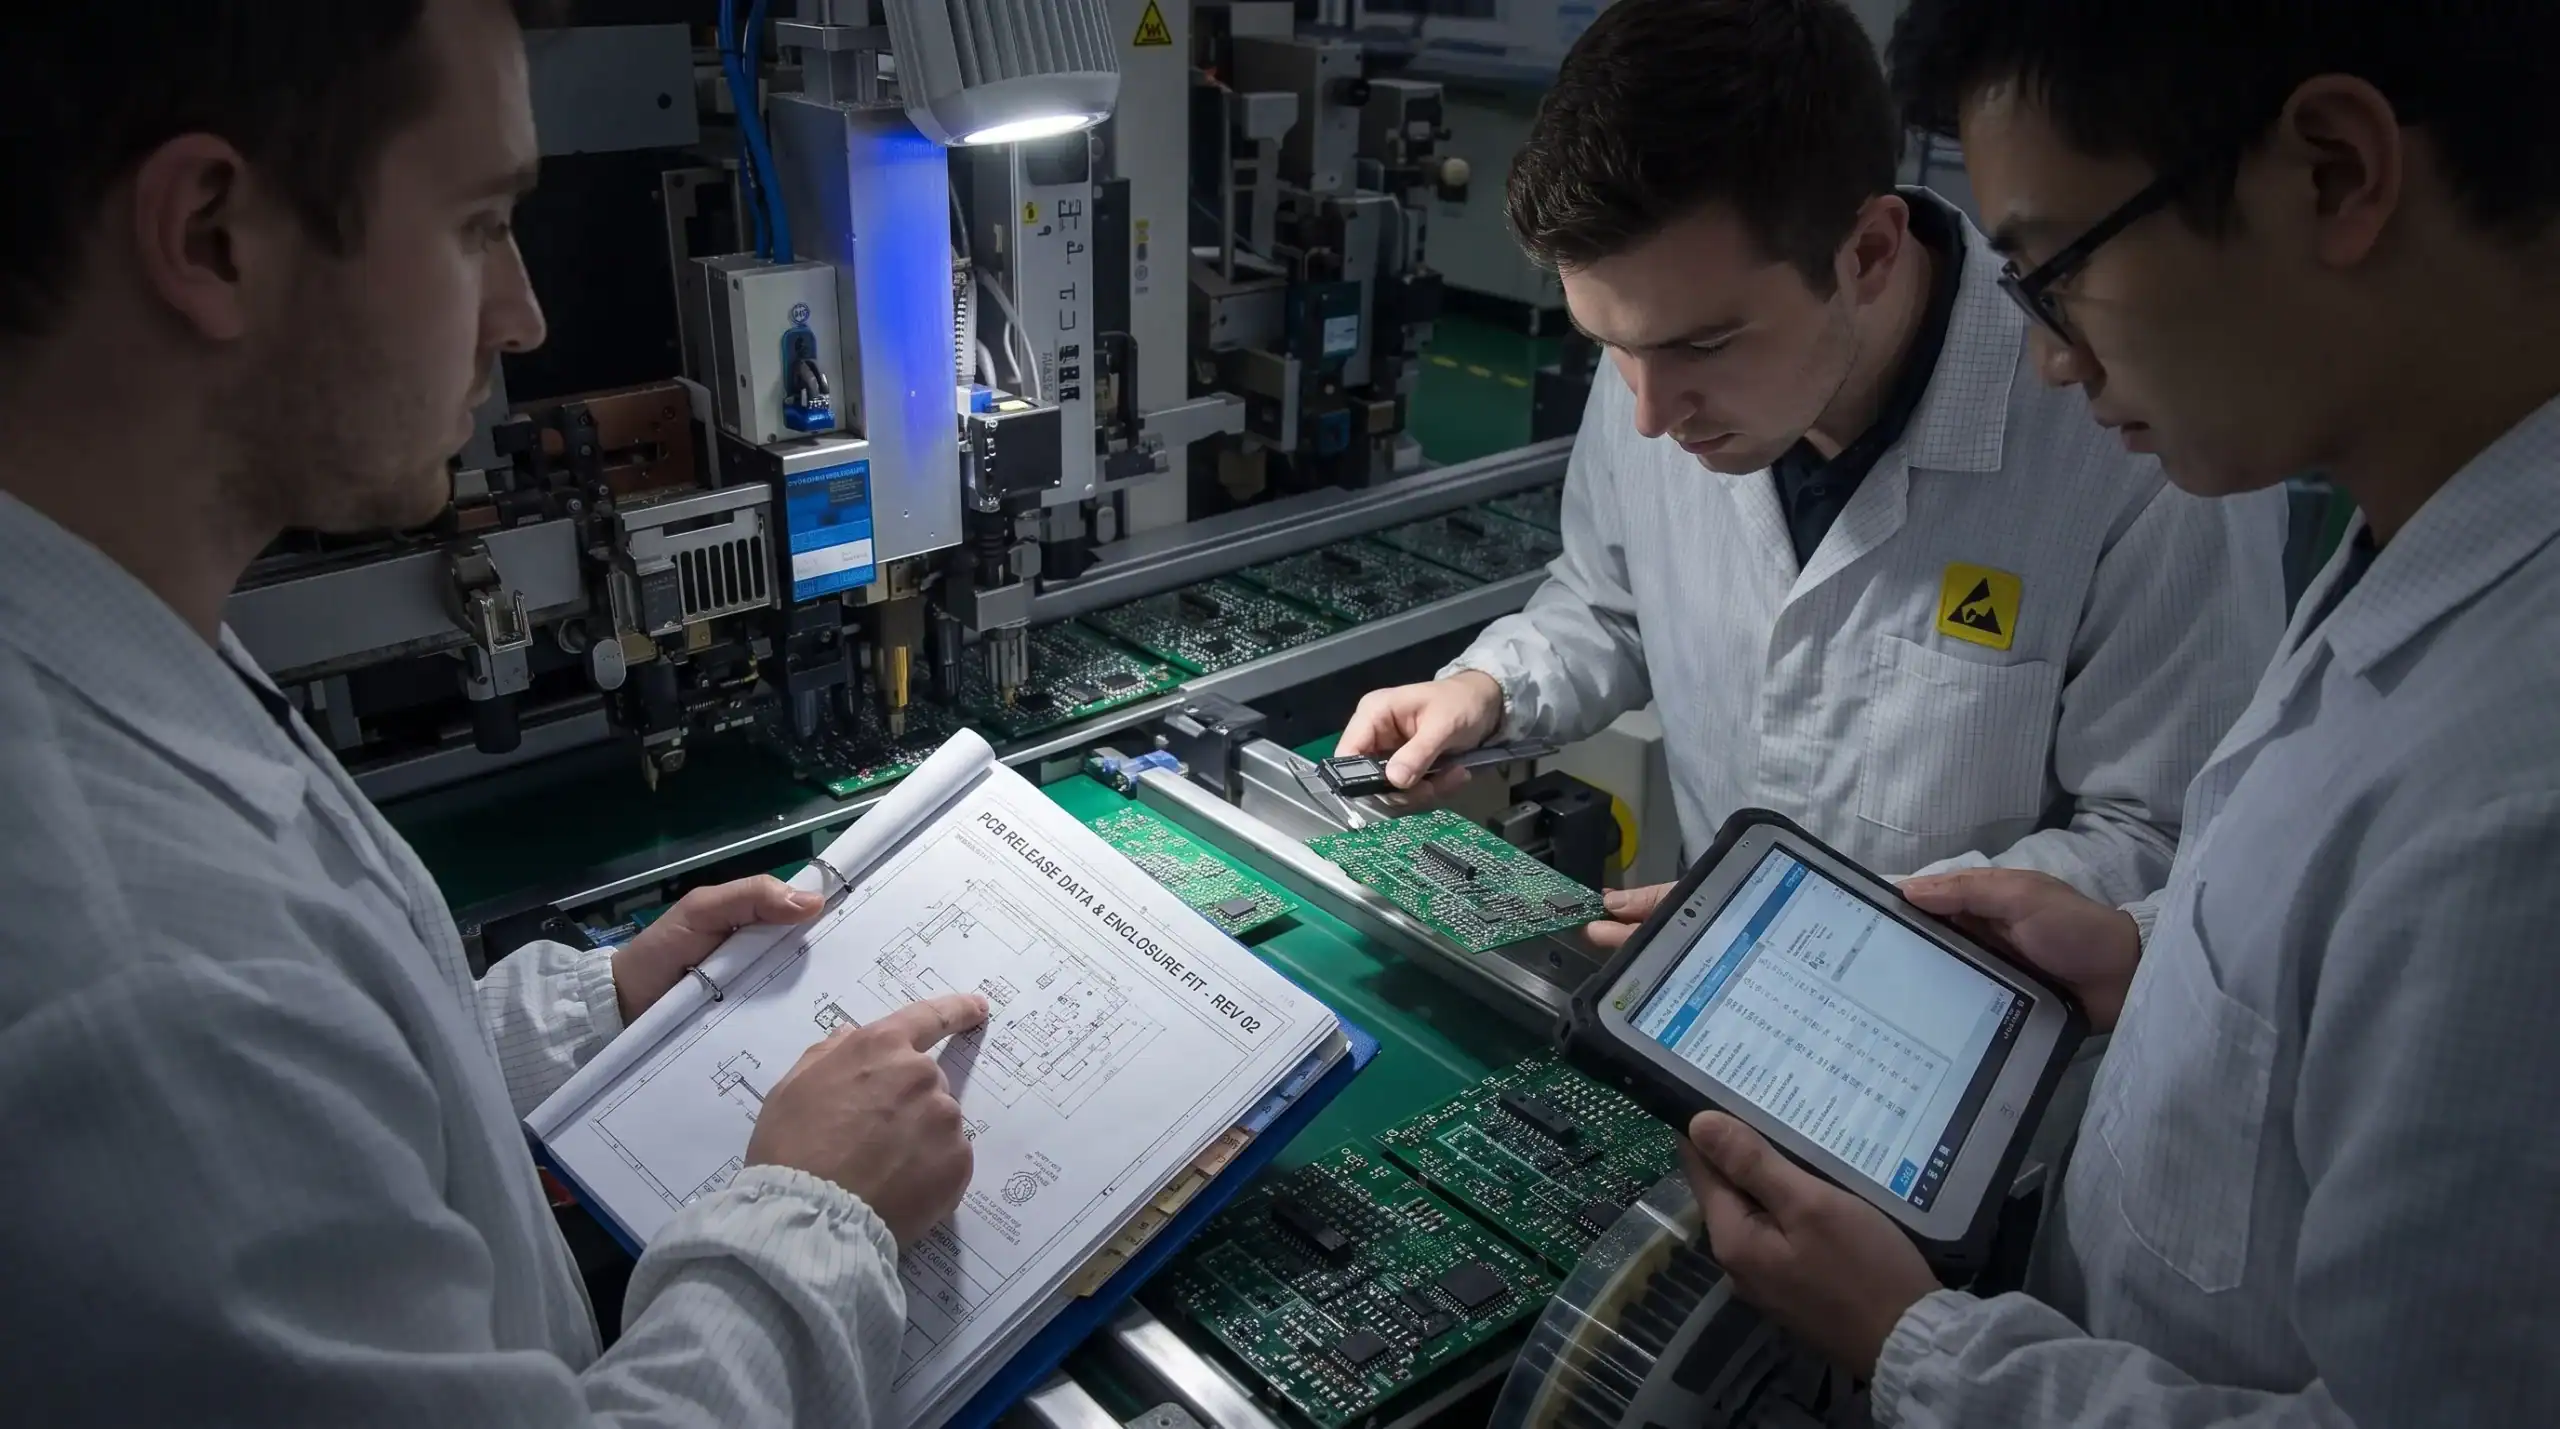
Review quality improves when the team reviews intent, not just geometry. It is useful to ask why noisy and sensitive circuits are placed where they are, why a particular stack-up was chosen, how heat leaves the board, how the product will be tested and how the design will behave outside the laboratory.
Prepare prototype CAD data with volume build in mind
Prototype boards are often used to learn, but they should not teach the wrong lessons. A prototype that works only because it ignores the eventual enclosure, production process or compliance context can create false confidence. When the product moves towards pilot or volume build, those shortcuts may become revision errors.
If a prototype deliberately uses relaxed constraints, substitute parts, extra debug headers or oversized boards, those deviations should be documented. The team should know which prototype features are temporary and which are intended for production. This avoids the common situation where a proof-of-concept layout quietly becomes the basis for a product, despite not being designed for long-term manufacture.
A production-ready CAD package should support fabrication, assembly, inspection, test and lifecycle management. It should include consistent outputs, controlled revisions and enough documentation for suppliers to build the board without informal knowledge from the design team. ProMicro covers this transition in more detail in its guide on how to prepare a PCB design for prototyping and volume build.
How integrated engineering reduces CAD revision risk
The most effective PCB CAD design practices are not isolated layout techniques. They come from system-level thinking. A reliable board depends on how electronics, embedded software, analogue behaviour, power architecture, enclosure design, manufacturing constraints and compliance expectations interact.
This is why many costly revision errors occur at the boundaries between disciplines. A wireless module is placed correctly according to its datasheet, but the enclosure compromises antenna performance. A power converter is electrically functional, but its switching current loop creates EMC problems. A sensor front end measures accurately on the bench, but suffers from noise when integrated with a motor drive. A PCB is manufacturable, but difficult to test in production.
For companies developing high-value technical products, the goal is not simply to produce a PCB file. The goal is to create electronics that can be tested, certified, manufactured, maintained and supported over time. That requires early attention to hidden requirements, not only the explicit feature list.
An integrated development partner can help by challenging assumptions before they become layout decisions. That includes reviewing the product context, selecting suitable components, defining CAD constraints, planning EMC behaviour, considering enclosure effects, preparing prototypes and supporting the path towards manufacturing. The value is not only extra design capacity. It is risk reduction across the product lifecycle.
Frequently asked questions
What is PCB CAD design? PCB CAD design is the use of electronic CAD tools to create schematics, PCB layouts and manufacturing outputs for printed circuit boards. In professional product development, it also includes constraints, libraries, mechanical integration, documentation and release control.
Which PCB CAD errors most often cause board revisions? Common causes include wrong footprints, incomplete pin mapping, inadequate clearances, poor return paths, missing test points, mechanical misalignment and inconsistent release files. Many of these errors can be reduced through verified libraries, rule-driven design and staged reviews.
Can CAD design practices improve EMC performance? Yes. CAD decisions such as stack-up, component placement, return path control, grounding strategy, filtering location and cable interface layout strongly influence EMC behaviour. They do not guarantee compliance, but they help design with EMC risks in mind from the start.
When should manufacturability be considered in PCB CAD design? Manufacturability should be considered before layout begins. Track widths, drill sizes, component spacing, assembly access, test points, documentation and supplier capabilities all affect whether a design can move reliably from prototype to volume build.
Why involve mechanical and embedded software teams in PCB reviews? Mechanical teams can identify enclosure, connector, thermal and assembly constraints. Embedded software teams can confirm programming access, debug needs, boot behaviour and interface assumptions. Their input helps prevent revisions caused by system integration issues.
Reduce revision risk before the first board is ordered
If your product depends on reliable electronics, PCB CAD design should be treated as part of the full development process, not a standalone drafting task. The right constraints, reviews and release discipline can prevent expensive respins and help your team move from concept to production-ready hardware with fewer surprises.
ProMicro supports companies with embedded systems, power electronics, analogue electronics, PCB design, system engineering, prototyping and preparation for volume manufacturing. If you are developing a complex electronic product and want to reduce hidden technical risks early, contact ProMicro to discuss your project.