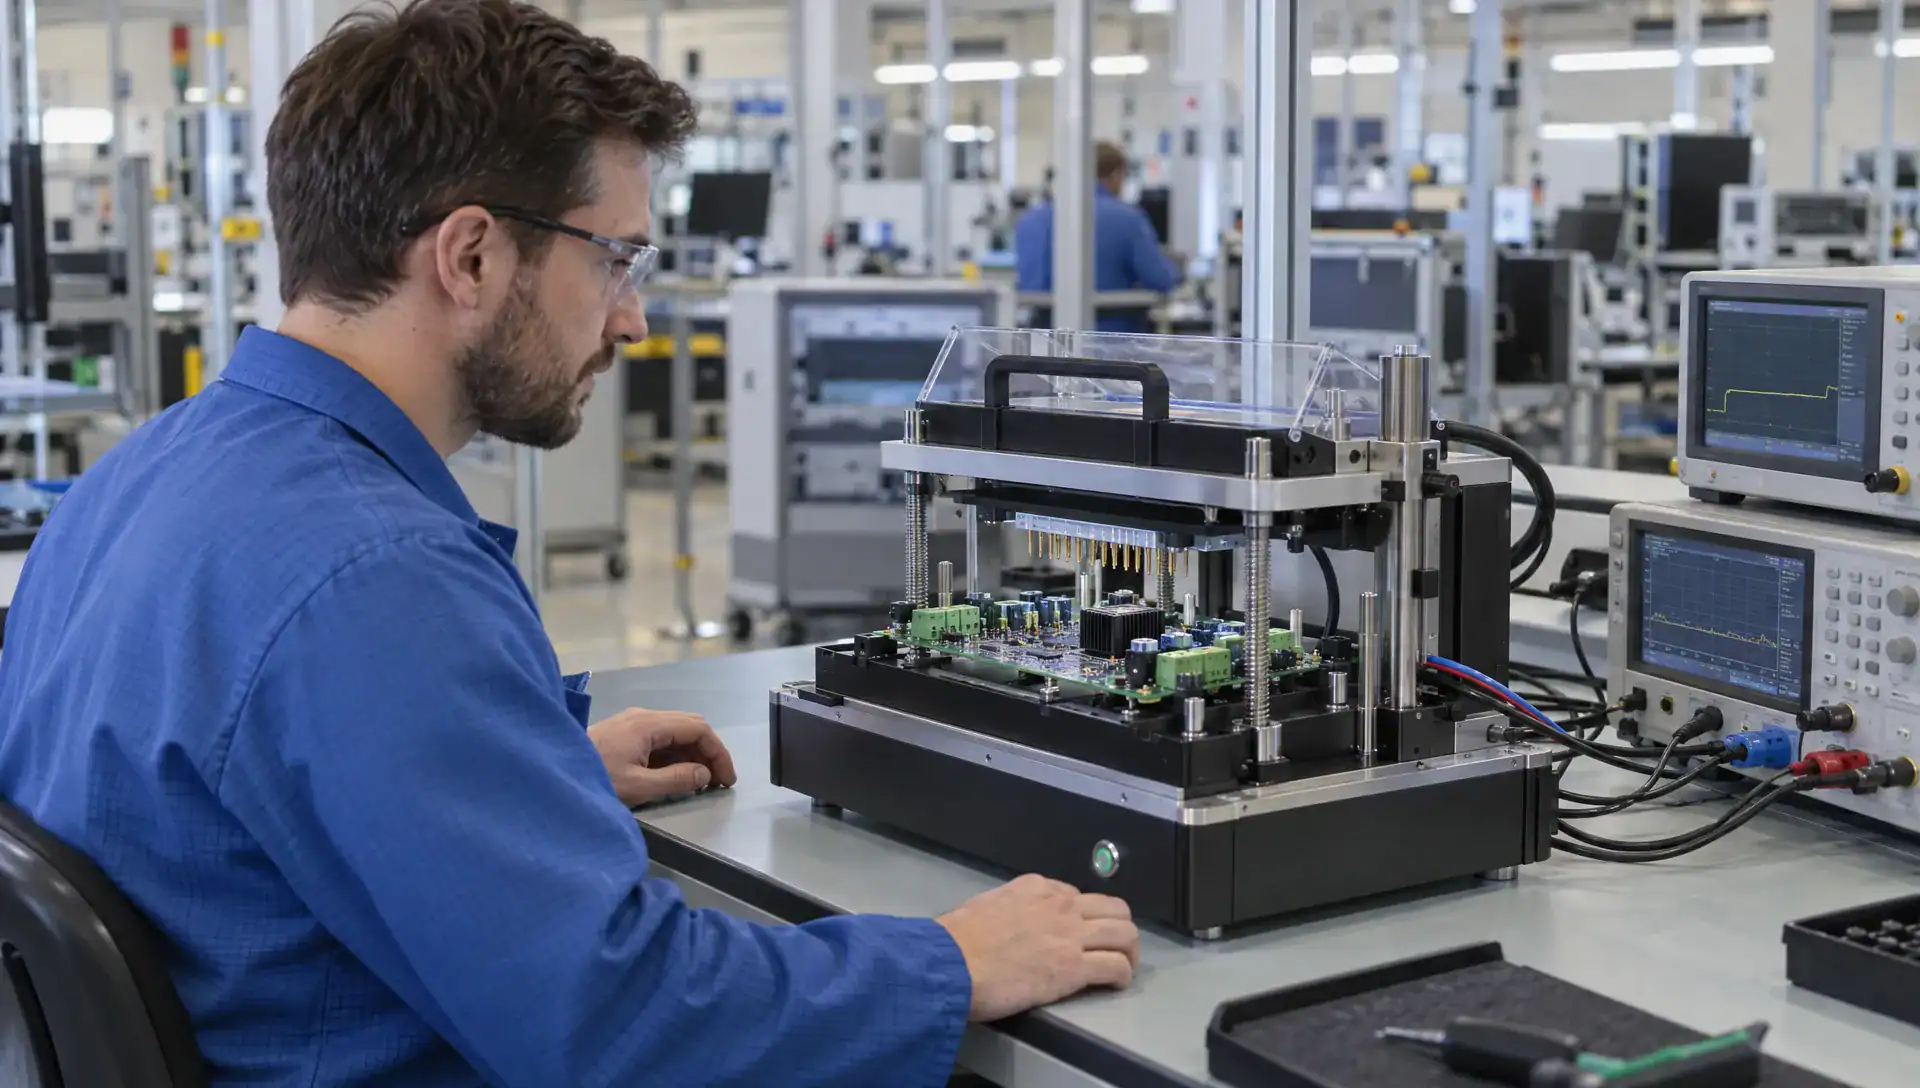
A printed PCB board designed for automated testing needs more than a row of accessible test pads. It needs a defined test strategy, controlled power-up, measurable acceptance criteria and firmware that allows the production station to exercise the hardware safely. Those decisions belong in the architecture and schematic reviews, not after the first assembly arrives.
Strictly speaking, the bare board is the PCB and the populated assembly is the PCBA. Most automated electrical testing discussed here applies to the assembly, but its effectiveness depends on choices made during PCB design. The objective is to detect manufacturing defects and verify critical functions without creating excessive fixture cost, test time or diagnostic ambiguity.
Define fault coverage before designing test access
Start with the faults that production testing must detect. For an industrial controller, these might include reversed components, missing connections, incorrect component values, defective power rails, programming failures or inaccurate sensor channels.
Separate manufacturing test coverage from design qualification. A production station checks each manufactured unit against defined requirements. It does not replace EMC assessment, environmental qualification, safety evaluation or verification of the product architecture.
Create a coverage matrix that connects each critical circuit or requirement to a test method, stimulus, measurement and acceptance limit. Record what remains untested rather than treating a successful boot sequence as evidence that the whole assembly works.
For a printed PCB board, this matrix should drive decisions about accessible nodes, isolation points, connectors and firmware hooks. Assign responsibility for each test to the board supplier, assembly partner or final product manufacturer. This avoids duplicated checks and gaps between suppliers.
Agree these requirements alongside the design-for-manufacturing review, while schematic and layout changes are still practical.
Select complementary test methods
No single test method provides complete coverage. Select a combination based on circuit complexity, assembly technology, expected volumes, fault risk and permitted cycle time.
| Method | Main contribution | Design implication |
|---|---|---|
| Automated optical inspection (AOI) | Checks visible placement, polarity and solder features | Consider component visibility and inspection access |
| Automated X-ray inspection | Examines hidden solder joints and internal connection features | Identify packages and joints that need inspection |
| Flying-probe testing | Measures accessible electrical nodes without a dedicated bed-of-nails fixture | Provide suitable probe access and measurement paths |
| Fixture-based in-circuit testing (ICT) | Checks accessible nets and selected component characteristics | Plan pad geometry, spacing, support and electrical isolation |
| Boundary scan | Checks supported digital interconnections through compatible devices | Confirm device support and accessible scan-chain connections |
| Functional testing | Exercises powered operation, interfaces and signal paths | Provide controlled stimuli, loads, observability and firmware support |
A printed PCB board may use flying-probe testing during early builds, then move to fixture-based testing as production requirements justify it. Functional testing can complement either approach.
Ask prospective test partners to assess coverage before layout release. A proposed test may be impractical because a node is inaccessible, a measurement is masked by parallel circuitry or the selected components do not support the assumed boundary-scan operation.
Design test access into the printed PCB board
Agree test-point rules with the fixture designer and assembly partner. There is no universal pad diameter or spacing that suits every probe type, fixture technology and board geometry.
Make probe contact repeatable
Dedicated test pads need suitable exposed copper, solder-mask clearance and a finish compatible with repeated probing. Avoid relying on solder-coated component leads as the only contact surface when a dedicated pad would provide more consistent access.
Where practical, keep probe access on one side. Two-sided fixtures are possible, but introduce additional mechanical constraints. Reserve clearance around tall components, connectors, mounting hardware and enclosure features that could obstruct probes.
Provide locating features and support positions so probe force does not bend the assembly excessively. Support matters near fine-pitch devices, connectors and other mechanically sensitive areas. Check accessibility after assembly, not just in the bare-board CAD view.
Expose the nodes that matter
Useful access commonly includes supply inputs, power rails, grounds, reset, programming signals, communication buses and selected analogue nodes. Separate force and sense connections where contact resistance would otherwise distort a low-resistance measurement.
For a printed PCB board with high-speed or sensitive analogue circuitry, adding a test pad can change the circuit being measured. Pads, vias and routing branches introduce parasitic effects. Use suitable access structures, buffered observation points or indirect measurements where direct probing would compromise operation.
Engineer safe power-up and fault containment
The station must handle incorrectly assembled boards, not just functioning ones. Define what happens if the supply is shorted, a regulator is damaged or an output starts unexpectedly.
Begin with appropriate unpowered checks, followed by controlled energisation. Specify supply sequencing, current limits, enable states and conditions that stop the test. Stored energy must be discharged safely before handling or repeat measurements.
For power electronics, define the load and energy path explicitly. A motor-drive output may require a controlled electrical load rather than a freely moving motor. High-energy or hazardous-voltage testing requires suitable guarding, interlocks and safe measurement equipment.
The printed PCB board should provide a way to hold power stages and actuators in a safe state until the station deliberately enables them. Check behaviour before firmware starts and during resets, communication loss or programming interruptions.
Review grounding between the unit under test, fixture, oscilloscope and other instruments. An earth-referenced measurement connection can unintentionally short a floating node. Isolation choices must follow the actual circuit and hazard assessment, not simply the connector arrangement.
Build production-test support into embedded firmware
Firmware should make hardware functions observable without allowing a test result to conceal the defect being investigated. For example, successful communication with a sensor does not prove that the sensor input path is accurate.
Define a documented production-test interface with commands for reading measurements, controlling outputs, checking memory, exercising communication links and reporting firmware identity. Provide time-outs, error codes and deterministic responses so the station can distinguish a device fault from a communication failure.
For a printed PCB board with several power domains or peripheral devices, report intermediate results rather than one overall pass flag. That makes failures easier to diagnose and helps reveal whether a problem follows a component batch, assembly process or design revision.
Production access also needs a security policy. Decide how test mode is entered, which commands remain available after shipment and how programming credentials are protected. Confirm that locking or provisioning a device does not make required rework impossible.
Where calibration is required, store coefficients with integrity checks and clear version information. Verify that the normal application uses them correctly, rather than accepting a successful write operation as proof of calibration.
Set measurement limits and an acceptance rule
Every automated measurement needs defined operating conditions. Specify supply voltage, load, stimulus, settling time, temperature assumptions and the relevant measurement point.
Avoid copying a nominal component value directly into a pass/fail threshold. The measured result may include component tolerances, contact resistance, fixture wiring, instrument error, noise and temperature effects. Analogue paths may also need time to settle after switching test channels.
Consider an illustrative printed PCB board with a 3.3 V rail specified within ±5%. Its specification limits are 3.135 V and 3.465 V. The station’s acceptance limits need a documented decision rule that accounts for measurement uncertainty. Simply accepting every displayed value inside the specification range can create uncertainty near either boundary.
Guard bands can reduce the risk of accepting an out-of-specification unit, but may also reject good units near a limit. Select that trade-off deliberately.
Distinguish product limits from process-monitoring limits. A measurement can meet the product requirement while drifting enough to justify investigation. Retain numerical results, not only pass/fail outcomes, so the production team can identify those changes.
Develop a test sequence that isolates faults
Consider a hypothetical 24 V industrial controller with a microcontroller, analogue inputs, a current-sensing circuit and a switched output. Its sequence should establish safe prerequisites before moving to more energetic tests.
- Confirm identity and setup: Check the assembly revision, fixture configuration and permitted firmware package before applying power.
- Perform unpowered checks: Check selected shorts, connections and component characteristics using methods appropriate to the circuit.
- Apply controlled power: Monitor input current and verify critical rails before enabling higher-energy functions.
- Program and verify: Load the approved firmware, verify its identity and check that the device starts consistently.
- Exercise signal paths: Apply known analogue inputs, exchange communication messages and test outputs against defined loads.
- Calibrate and close: Where required, calculate calibration values, verify performance at separate check points and confirm the final shipping configuration.
On this printed PCB board, checking analogue inputs at several meaningful levels gives better evidence than reading a single zero-input value. Similarly, an output may need verification both when enabled and when disabled to detect a stuck-on condition.
Define failure handling at every stage. The station should stop safely, preserve diagnostic data and identify the failed operation. Do not allow automatic retries to turn intermittent contact or hardware faults into unexplained passes.
Validate the test station as well as the product
A faulty station can reject good assemblies or repeatedly accept defective ones. Validate the fixture, instruments, switching paths, test software and configuration as a complete measurement system.
Use known-good assemblies to establish repeatability, but do not rely on them alone. Challenge the station with controlled faults or representative faulty units where safe and practical. Confirm that each intended check can detect the defect assigned to it.
For the printed PCB board under test, repeat measurements across different operators, fixture insertions and representative units. Investigate results that change significantly after reseating. Contact wear, contamination, board movement and electrical noise can all affect repeatability.
Define fixture maintenance, instrument calibration and station self-checks. Revalidate affected tests after changes to probes, cabling, instruments, software or firmware.
Track first-pass yield separately from yield after retest or rework. A rising retest rate may indicate deteriorating contact quality even when the final acceptance rate appears stable. Production data should help distinguish product defects from measurement-system problems.
Release a controlled test package for manufacturing
The manufacturing handover needs more than PCB fabrication files and a schematic. Supply a controlled test-point map, accessible-net information, mechanical fixture constraints, programming connections and the relevant assembly variants.
Include the test specification, approved firmware identifiers, command definitions, acceptance limits, calibration procedure and required shipping state. Define which results must be retained and how they link to the unit serial number or production batch.
A printed PCB board revision can affect test coverage even when the product’s external behaviour remains unchanged. Moving a pad, changing a component value or updating a bootloader may require changes to fixture hardware, test software or limits. Maintain a compatibility record across board, firmware and station revisions.
Pilot builds should verify both the product and the manufacturing test process before release. This is an important part of the transition from prototype to volume production, rather than an activity postponed until a production problem appears.
Finally, document residual coverage gaps. Product owners need to know which risks are controlled through production testing and which depend on design verification, supplier controls or qualification evidence.
Frequently asked questions
Does every PCB need a bed-of-nails fixture? No. Flying-probe testing, programming fixtures and functional test stations may provide a better fit for some assemblies. Select the approach using coverage needs, access constraints, expected volumes and cycle time.
Can automated functional testing replace ICT? Sometimes, but only where the agreed coverage supports that decision. Functional tests can miss assembly defects that do not immediately affect operation. ICT also has limitations, so compare the faults each method can detect.
Does passing an automated test prove compliance? No. A production test verifies selected characteristics under defined conditions. It does not establish EMC, radio, safety or other regulatory compliance by itself.
When should test engineering start? Before schematic and layout release. Planning test access for a printed PCB board early gives hardware, firmware, mechanical and manufacturing teams time to resolve constraints without a late redesign.
Bring testability into the development review
Reliable automated testing depends on coordinated electronics, embedded firmware, mechanical integration and manufacturing decisions. The useful starting point is a review of critical functions, likely faults, proposed coverage and safe test conditions.
ProMicro supports electronics development through embedded systems, power electronics, analogue design, PCB design, prototyping and manufacturing preparation. Bringing testability into that work early helps teams identify coverage gaps, reduce avoidable redesign and prepare a more controlled route to repeatable production.